Hey there, if you’ve ever worked with carbon steel turned parts (and I’m guessing if you’re here, you either do, or you’re sourcing them), you’ve probably found yourself asking the same question: “What’s the actual hardness range I need here? Too soft, and the part will wear out in a week; too hard, and it’ll crack before you even finish machining it.” As a carbon steel turned parts supplier who’s been on the grind for 12 years, I’ve answered this a hundred times, and it’s not a one-size-fits-all answer—let’s break it down like we’re chatting over a cuppa, no stuffy textbook jargon. Carbon Steel Turned Parts

First, let’s get real about what carbon steel even is, because that’s the foundation. Carbon steel is basically iron with a little carbon (usually between 0.05% and 2.1% by weight) mixed in—no extra elements like chromium or nickel to make it stainless, which is why it’s cheaper, stronger, and way more common for turned parts than alloy or stainless steel. The amount of carbon is the big driver of hardness, right? Low carbon (less than 0.3% C) is soft, medium (0.3% to 0.6% C) is middle-of-the-road, high carbon (over 0.6% C) is hard as nails. But wait, when we’re talking turned parts, we’re not just talking raw carbon steel—we’ve got to factor in how we made the part, because turning is a machining process, not just forging or casting. Turning cuts, shapes, and machines the steel into precise parts, and that machining can actually affect the hardness of the surface, not just the core.
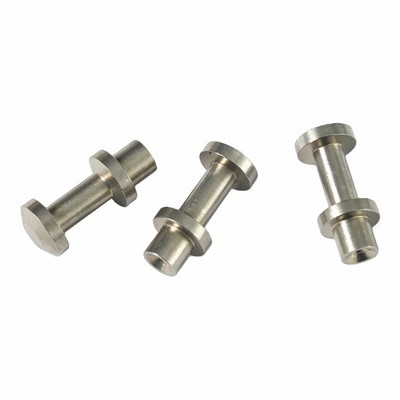
Let’s start with low carbon steel turned parts, because that’s what most people ask about first for things like bolts, pins, or brackets that need to bend a little instead of breaking. Low carbon steel (aka mild steel, if you’ve heard that term) usually sits at a hardness range of about 100 to 150 HRB (that’s Rockwell B scale, for anyone who’s not a metallurgy nerd—HRB is used for softer metals; HRC is for harder stuff). Wait, but if you machine low carbon steel without any heat treatment, it’s around 100 HRB, but if we do a little work hardening during turning (that’s when the metal gets harder as you cut it, because the bits get bent and stretched), the surface can jump to 120-150 HRB. Now, why does that matter? If you’re making a part that needs to be drilled into or attached to something, low carbon is great because it’s ductile. But if you use it for a part that needs to resist wear, like a bushing, you’re going to want to case harden it—add a little carbon to the outer layer, so the surface gets up to 60 HRC, while the core stays soft. But that’s a heat treatment step, not the raw hardness right out of turning. Medium carbon steel is the workhorse, honestly. For medium carbon (0.3% to 0.6% C) turned parts, the as-machined hardness is usually 150 to 250 HB (Brinell scale, another common one; HB is good for mid-range hardness). But here’s the thing—most medium carbon parts get heat treated after turning, right? We call that quenching and tempering. Quenching is heating the steel up fast and cooling it quick, which makes it hard, then tempering is heating it a little lower to take the edge off so it doesn’t crack. So if you temper it at a low temperature (like 200°C), you get a hardness range of 50 to 58 HRC—super strong, good for gears, shafts, or things that need to handle torque. If you temper it a little higher, like 400°C, it’s softer, around 30 to 40 HRC, which is better for parts that might get hit or bent a little, like axles or connecting rods. I always tell my clients: if your part is going to see a lot of friction and force, aim for 50-58 HRC. If it’s for something that needs a little give, 30-40 HRC is the sweet spot. Now high carbon steel—this is the stuff for when you need maximum hardness, like springs, cutters, or bearings. As-machined high carbon (over 0.6% C) is around 200 to 250 HB, but after quenching and tempering, it can hit 55 to 65 HRC. Wait, but high carbon is tricky—if you quench it too fast, it’s prone to cracking, especially when you’re turning it, because the machining process can create tiny stress points. That’s why I always work with my clients to adjust the turning parameters—slower speeds, sharper tools, so we don’t create extra stress that’ll make the part crack after heat treatment. But here’s a common myth I have to bust: hardness isn’t everything. I’ve had clients come to me asking for the hardest possible steel for a part, only to find out it’s going to be installed in a place where it’ll flex, and the hard steel would snap. Like, last year, a guy wanted high carbon for a set of agricultural plow blades—they kept breaking because he went too hard. We switched to medium carbon, tempered to 45 HRC, and they lasted twice as long. That’s the thing about hardness ranges for carbon steel turned parts: it’s not just about the steel grade, it’s about the application, the machining process, and the heat treatment you choose. Let’s also talk about the turning process itself, because I’m a supplier, so I know this firsthand. When we turn carbon steel, the cutting tool is removing material at high speed, which generates heat. That heat can make the surface of the steel harder—work hardening, like I mentioned earlier. For example, if you’re turning low carbon steel at too high a speed, you can get a surface hardness of 160 HRB, which is way higher than the core. That might sound good, but it can make the part brittle on the surface, or even wear out the cutting tool faster. We adjust our feeds and speeds depending on the grade: for low carbon, we use a higher feed and slower speed, for high carbon, lower feed and higher speed with coolant to keep the heat down, so we don’t get uneven hardness. Another thing: tolerance. When you’re machining turned parts, the hardness can affect how tight we can hold the tolerances. Harder steel is less likely to deform after machining, which is great for parts that need to fit exactly. So if you need a part that’s within 0.001 inches, a medium or high carbon steel tempered to 40-50 HRC is perfect, because it won’t shift after turning. Low carbon steel is softer, so it can deform a little, which is fine if you’re not dealing with super tight tolerances, like a bracket that’s bolted on, not precision fit. Wait, let’s get specific with examples, because that’s what people care about. Let’s list common parts and their typical hardness ranges, right from our shop floor: 1. Low carbon steel turned parts (bolts, pins, brackets): As-machined: 100-150 HRB. If case hardened (for wear resistance): Surface 55-60 HRC, core 100-120 HRB. 2. Medium carbon steel turned parts (gears, shafts, axles): As-machined: 150-250 HB. Heat treated (quench/temper): 30-58 HRC depending on temper temp (low temper = higher HRC). 3. High carbon steel turned parts (springs, bearings, cutters): As-machined: 200-250 HB. Heat treated (quench/temper): 55-65 HRC. But like I said, these ranges are flexible. If a client needs a gear that has to handle a lot of torque, we’ll aim for 55-58 HRC. If they need a shaft that has to fit into a bearing without seizing, we might go a little softer, 45-50 HRC, so it can wear a little instead of damaging the bearing. What about common mistakes I see? Clients asking for a one-size-fits-all hardness, or not considering the post-machining process. For example, if you’re buying turned parts and then you’re going to drill or tap them after, you don’t want them too hard—because tapping a 55 HRC steel is way harder than tapping a 30 HRC one, and you’ll break the tap. We always check in with our clients before we start machining: “What are you doing with this part after we make it? Any other processes like tapping, grinding, or heat treatment?” That way, we can adjust our turning parameters and the initial hardness to make it easier for them, no extra work or broken parts. Another thing to note: hardness testing. We use a portable Rockwell tester on our shop floor, because it’s quick and accurate for turned parts, instead of sending samples out to a lab. That means we can guarantee the hardness range right when the parts are ready, no surprises. A lot of suppliers skip that, but we don’t—because if a part is too soft, it’ll wear out fast, and if it’s too hard, it’ll crack. We stand behind our parts, so we make sure the hardness is exactly what the client needs. So, to wrap this up: the hardness range of carbon steel turned parts isn’t a single number—it depends on how much carbon is in the steel, what the part is going to be used for, whether you’re doing any heat treatment after turning, and even how we machine it in our shop. For most applications, you’re looking at: Low carbon: 100–150 HRB (as-machined) / up to 60 HRC (case hardened) Medium carbon: 150–250 HB (as-machined) / 30–58 HRC (heat treated) High carbon: 200–250 HB (as-machined) / 55–65 HRC (heat treated) But if you’re not sure, don’t guess—reach out. I’ve been in this game long enough to look at your part design, what it’ll be used for, and tell you exactly what hardness range you need, so you don’t waste money on steel that’s too hard or not hard enough. If you’re sourcing carbon steel turned parts, or you have questions about hardness, machining, or heat treatment, don’t hesitate to connect. We can work out exactly what your parts need, and get you quotes fast with no hidden fees. Just send over your specs, and we’ll take care of the rest.
Aluminum Turned Parts References:
- ASTM A29/A29M, Standard Specification for Steel Bars, Carbon and Alloy, Hot-Wrought, and Cold-Finished, General Requirements for
- Kalpakjian, S., & Schmid, S. R. (2020). Manufacturing Processes for Engineering Materials (8th ed.). Pearson
- Groover, M. P. (2019). Fundamentals of Modern Manufacturing: Materials, Processes, and Systems (7th ed.). Wiley
Huizhou Quanyi Precision Hardware Products Co., Ltd.
We’re well-known as one of the leading carbon steel turned parts manufacturers and suppliers in China, featured by quality products and good service. Please rest assured to buy customized carbon steel turned parts made in China here from our factory. Contact us for more details.
Address: Building A10, 7th Floor, Zhongchuangyingke 5G Industrial Park, Zhonghan Industrial Park, Tonghu Town, Huizhou City
E-mail: info@qycncturning.com
WebSite: https://www.qycncturning.com/
